

- お役立ち記事
- Heat-affected zone control techniques to prevent post-weld cracking mismatch.
その単価は妥当か。
AI が根拠付きで分析。
相見積の比較も発注も進捗管理も、ひとつの画面に。

Heat-affected zone control techniques to prevent post-weld cracking mismatch.
目次
Understanding the Heat-Affected Zone
The heat-affected zone (HAZ) is a critical area in welding that requires careful attention to prevent post-weld cracking and mismatch.
This zone is the portion of the material that, while not melted, has experienced changes due to the intense heat of welding.
Understanding the heat-affected zone is crucial for ensuring the integrity and strength of welded structures.
The Importance of Controlling the Heat-Affected Zone
Controlling the heat-affected zone is essential for maintaining the quality and durability of welds.
Improper management of this zone can lead to post-weld defects such as cracking, which can compromise the safety and performance of the welded component.
Factors Affecting the Heat-Affected Zone
Several factors influence the characteristics of the heat-affected zone, including the type of material, the welding process used, and the parameters set during welding.
Materials with different thermal conductivity, such as steel and aluminum, will have different HAZ behaviors.
Therefore, it is crucial to consider these factors when planning and executing welding tasks.
Techniques for Controlling the Heat-Affected Zone
To prevent post-weld cracking and ensure proper matching, there are several techniques that can be employed to control the heat-affected zone effectively.
Preheating the Material
Preheating involves raising the temperature of the base material before welding.
This technique lowers the thermal gradient between the weld metal and base metal, reducing the risk of cracking in the heat-affected zone.
Preheating is particularly useful for high-carbon steels and thick sections where rapid cooling can be problematic.
Post-Weld Heat Treatment
Post-weld heat treatment (PWHT) is a technique used to relieve residual stresses and reduce hardness in the heat-affected zone.
By heating the welded component to a specific temperature and then cooling it at a controlled rate, PWHT minimizes the likelihood of cracking and distortion.
This technique is often used for pressure vessels and critical structural applications.
Controlling Heat Input
Careful control of heat input is vital to minimize the size of the heat-affected zone and prevent overheating.
This can be achieved by adjusting welding parameters such as voltage, current, and travel speed.
Lowering the heat input reduces the amount of material affected by welding, minimizing the risk of cracking and mismatch.
Using Low-Hydrogen Electrodes
Low-hydrogen electrodes help to minimize hydrogen-induced cracking in the heat-affected zone.
Hydrogen can enter the weld pool and accumulate, leading to post-weld cracks.
By selecting appropriate low-hydrogen consumables and maintaining proper handling and storage, the risk of cracking can be significantly reduced.
Material Selection and Weld Design
Beyond the techniques specifically targeting the heat-affected zone, material selection and proper weld design play a crucial role in preventing post-weld cracking and mismatch.
Choosing Compatible Materials
Selecting materials that are compatible with each other is fundamental to avoiding mismatch issues.
Materials with similar thermal expansion rates and compatible mechanical properties are less likely to experience post-weld stresses that lead to cracking.
Optimizing Weld Design
A well-designed weld can greatly reduce the stress concentrations that contribute to cracking.
Design considerations such as joint geometry, weld size, and the direction of welding all influence the behavior of the heat-affected zone and should be assessed during the planning phase.
Monitoring and Inspection
Continuous monitoring and inspection throughout the welding process are essential to maintain control over the heat-affected zone.
Using Non-Destructive Testing
Non-destructive testing (NDT) methods like ultrasonic testing and radiography can detect defects and assess the integrity of the weld and the heat-affected zone.
Regular inspections can identify areas at risk of cracking and allow for corrective measures to be implemented promptly.
Monitoring Temperature
Monitoring the temperature of the welding environment and the material itself provides valuable data for managing the heat-affected zone.
Using thermal cameras or temperature probes can help ensure that appropriate preheating and post-weld heating procedures are properly executed.
Conclusion
Effective control of the heat-affected zone is vital to prevent post-weld cracking and mismatch.
By employing techniques such as preheating, post-weld heat treatment, controlling heat input, and selecting appropriate materials, welders can enhance the quality and reliability of their work.
Through careful planning, monitoring, and inspection, the risks associated with the heat-affected zone can be mitigated, resulting in safer and more robust welded structures.
この記事の理解を深める
無料ホワイトペーパーをプレゼント
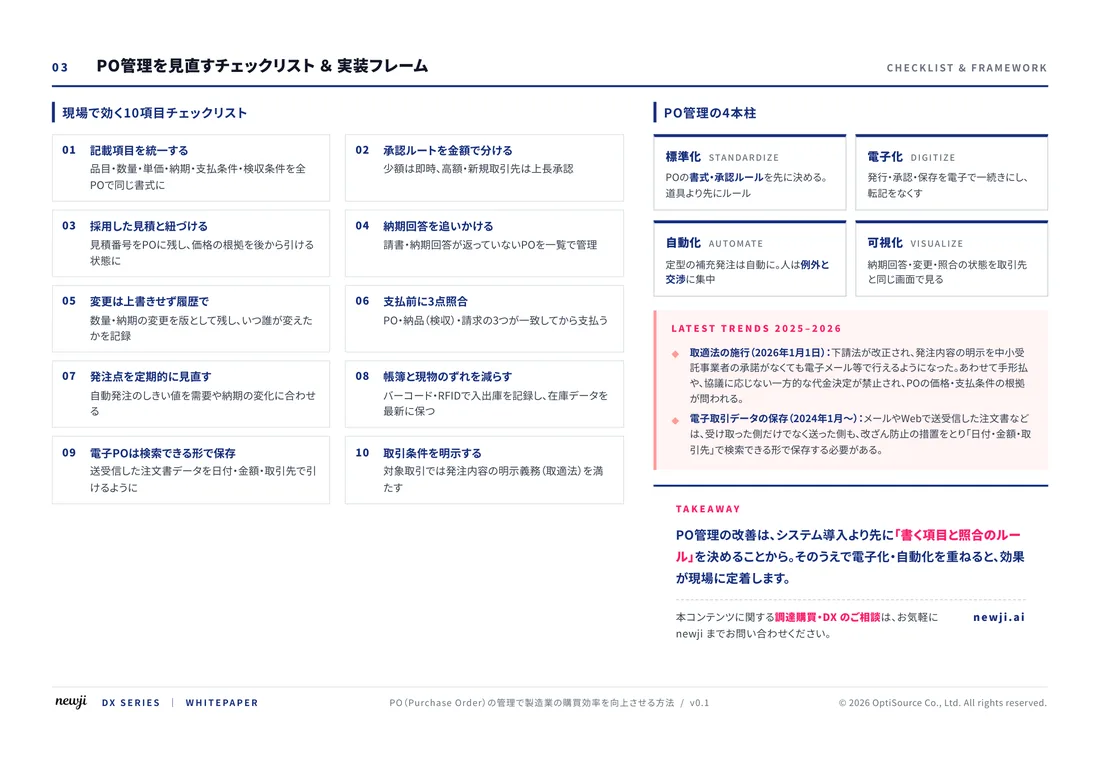
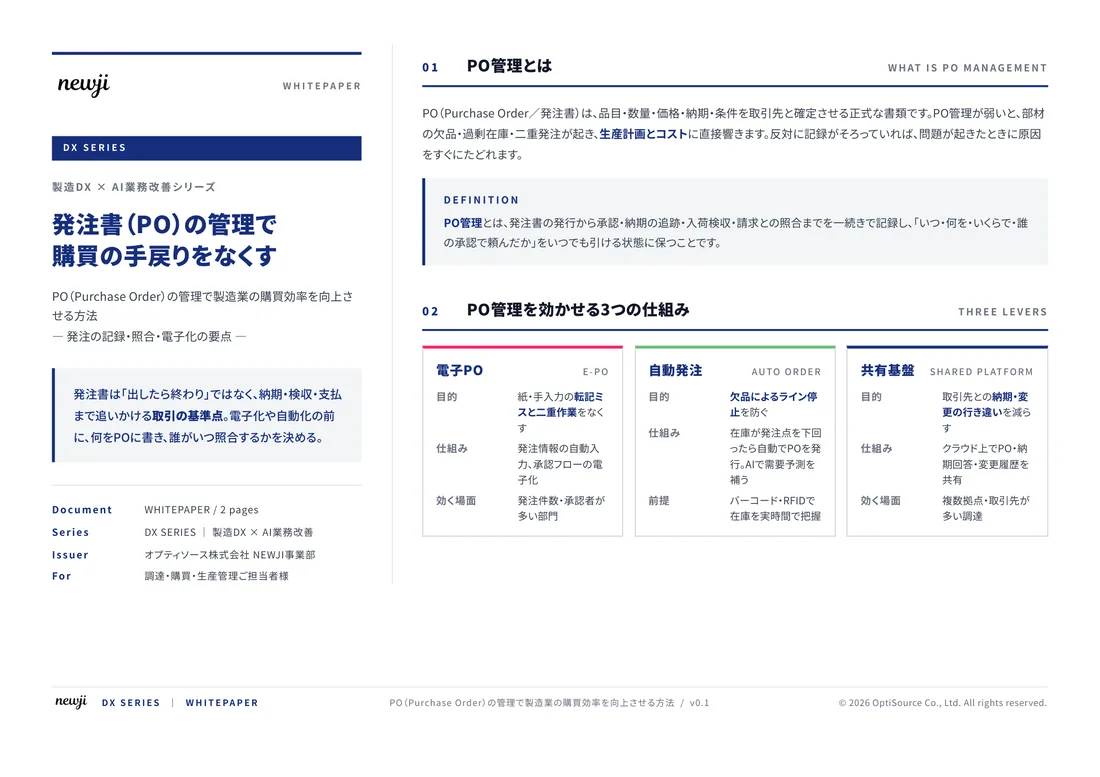
製造業の現場で使える実務資料(PDF)を無料でお届けします。"こんな資料が届きます" ↓ 下のボタンからどうぞ。
FREE DOCUMENT — サービス資料(PDF・無料)
製造業の見積・受発注クラウド
「Newji one」とは
Newji one は、製造業の調達・受発注に特化したクラウド/AIエージェント。見積依頼・発注書作成・進捗管理・承認をひとつの画面に集約し、AIが比較と異常検知を担当。最後の「GO」だけ人が押す仕組みです。
▶ 製造業の見積・受発注クラウド「Newji one」を、資料で見る(PDF・無料)
- 見積〜発注〜納期を一元管理。催促・転記のムダをゼロに
- AIが相見積もり比較と異常検知。あなたは判断だけに集中
- 取引先は「招待」で完全無料。自社コストだけで取引先ごとデジタル化
※ 取引先から招待された企業様は完全無料でご利用いただけます
 NEWJI総研
 OEM/ODM 生産委託
 AI/DX支援
 見積・発注クラウド Newji one
受発注が増えるほど、入力・確認・催促が重くなる。
受発注管理を“仕組み化“して、ミスと工数を削減しませんか。
見積・発注・納期まで一元管理できます。